How to Improve Material Utilization in IBM Production
Practical ways to improve material utilization in injection blow molding: preform and mold design, process control, regrind management and material handling.
The short answer
Injection blow molding already wastes little material because it produces no flash. Utilization improves further by right-sizing preform and wall thickness, keeping process settings stable so fewer bottles are rejected, drying and handling resin correctly, and reusing clean regrind where the application allows it.
On this page
Resin is usually the largest single cost in bottle production, so every gram that ends up as scrap, rejects or overweight bottles goes straight to the bottom line. Injection blow molding (IBM) starts with an advantage: the bottle is formed from an injected preform with a finished neck, so there is no flash, tail or pinch-off to trim. The remaining gains come from how the bottle, the mold and the process are managed.
This guide covers the practical levers that improve material utilization in injection blow molding production, from bottle design to daily process control.
Design the bottle and preform for the weight you need
Most material is decided before the first shot. A bottle that is heavier than its function requires will stay heavy for its whole production life.
- Set a target weight from function, not habit. Define the drop, top-load, squeeze and barrier requirements, then remove material that does not contribute to them.
- Design the preform for even stretch. In IBM the wall distribution is set by the preform shape and the core rod. A well-proportioned preform lets the body be thinned evenly instead of leaving thick corners and heavy bases.
- Avoid unnecessary thickness at the neck and base. The neck must stay accurate for sealing, but over-thick shoulders and bases are common sources of hidden excess weight.
- Standardize neck finishes and closures. Fewer neck variants mean fewer molds, fewer start-ups and less start-up scrap.
Our guide to how wall thickness is controlled in injection blow molding explains how preform design and temperature work together.
Keep the process stable to reduce rejects
Every rejected bottle consumes the same resin as a good one. Stable processing is therefore one of the cheapest ways to improve utilization.
- Control shot weight. Consistent melt temperature, screw recovery and injection pressure keep bottle weight inside a narrow band, so you can run close to the target weight instead of adding a safety margin.
- Stabilize temperatures. Preform, core rod and blow mold temperatures directly affect wall distribution and shrinkage. Drift here shows up as thin spots, warping or poor neck dimensions.
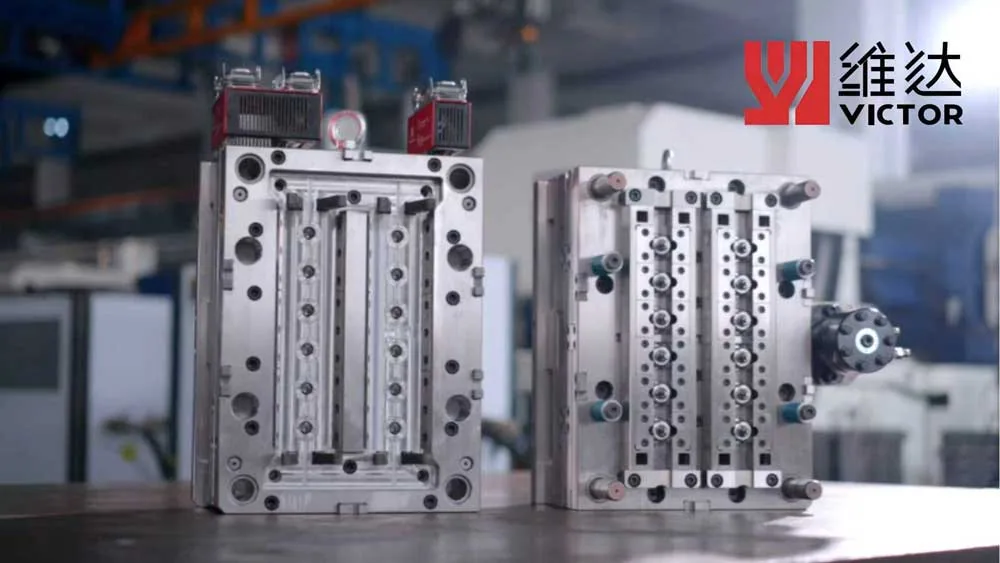
- Balance multi-cavity molds. In multi-cavity production, one weak cavity can create a steady stream of rejects. Check cavity-to-cavity weight and dimensions regularly.
- Shorten start-ups and changeovers. Record proven settings for each mold so production reaches stable quality in fewer cycles.
Handle resin and regrind correctly
- Dry and store resin as the supplier specifies. Moisture and contamination cause surface defects and weak spots that become rejects.
- Use first-in, first-out storage and keep hoppers covered to avoid contamination and color mix-ups.
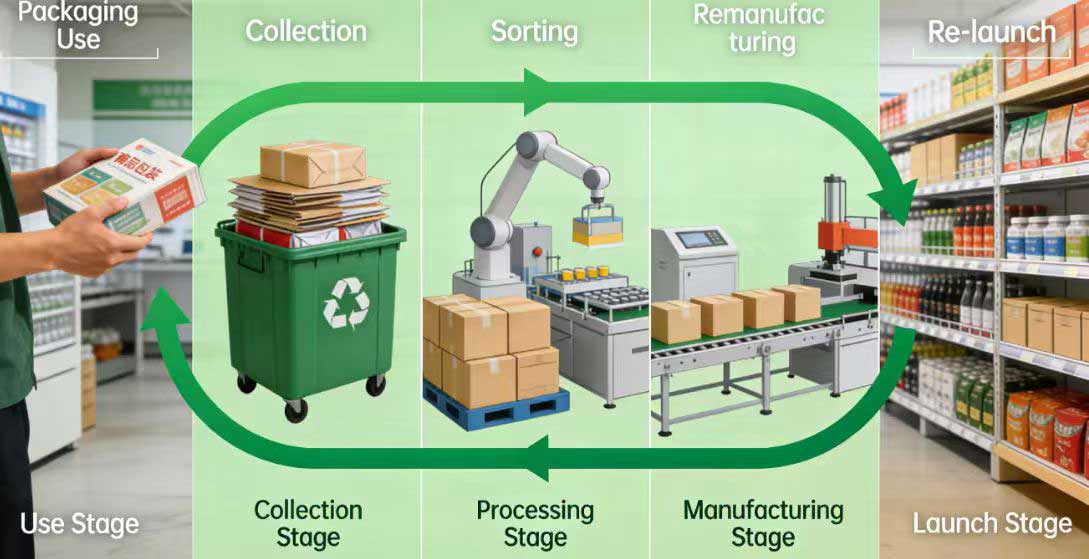
- Reuse clean regrind where the application allows it. Start-up bottles and rejects from the same resin can often be ground and blended back at a controlled ratio for non-critical products. Pharmaceutical and food-contact bottles may have stricter rules, so confirm what your customer and regulations permit.
- Keep colors and grades separate. Mixed regrind is usually unusable regrind.
Maintain molds and core rods
Worn or dirty tooling slowly pushes the process out of its window. Damaged parting lines create defects, blocked cooling channels change wall distribution and worn core rods affect neck accuracy and preform transfer. A planned cleaning and inspection routine keeps the mold producing good bottles at the target weight. See how to extend injection blow mold service life.
Measure what you waste
You cannot improve what you do not measure. A simple material balance for each mold and shift shows where losses occur:
- Resin issued to the machine versus the weight of good bottles produced
- Start-up scrap, process rejects and quality rejects, recorded separately
- Average bottle weight against the target weight
- Regrind generated and regrind reused
Even basic production data, collected consistently, quickly shows whether losses come from bottle design, start-ups, process drift or a particular cavity.
Train operators and share the results
Operators decide how quickly a machine is stabilized, how rejects are handled and whether regrind stays clean. Clear setup sheets, training on the reasons behind each setting and visible scrap figures for each line turn material efficiency into a daily habit rather than a one-off project.
Conclusion
Injection blow molding already avoids the flash waste of other blow molding processes. To improve material utilization further, design the bottle and preform for the weight you actually need, keep the process and molds stable, handle resin and regrind with discipline, and measure losses by mold and shift. Victor can review your bottle drawing, resin and target weight to suggest preform, mold and machine settings that use less material.
Frequently asked questions
Does injection blow molding produce less scrap than extrusion blow molding?
Usually yes. Injection blow molding forms the neck and body from an injected preform, so there is no flash, tail or pinch-off to trim. Extrusion blow molding normally produces trim scrap that must be reground. See our IBM vs EBM comparison.
Can regrind be used in pharmaceutical bottles?
It depends on the product and the customer’s quality and regulatory requirements. Many pharmaceutical and food-contact projects restrict or prohibit regrind, so confirm the rules before planning regrind use.
What is the fastest way to reduce material use on an existing bottle?
Start by measuring actual bottle weight against the target and by reducing rejects. Larger savings usually need a preform or bottle redesign, which should be validated with drop, top-load and sealing tests.
Plan your bottle project
Get a machine and mold recommendation for your bottle
Share your bottle drawing or sample, resin and target output. Victor's engineers will recommend a suitable MSZ model, cavity layout and mold concept.
Request a technical proposal- Bottle drawing, sample or photo
- Material: HDPE, PP, PS, PETG or other resin
- Target output and neck finish
- Destination country for delivery