SolutionsHousehold & chemical
In-mold labeled (IML) bottles
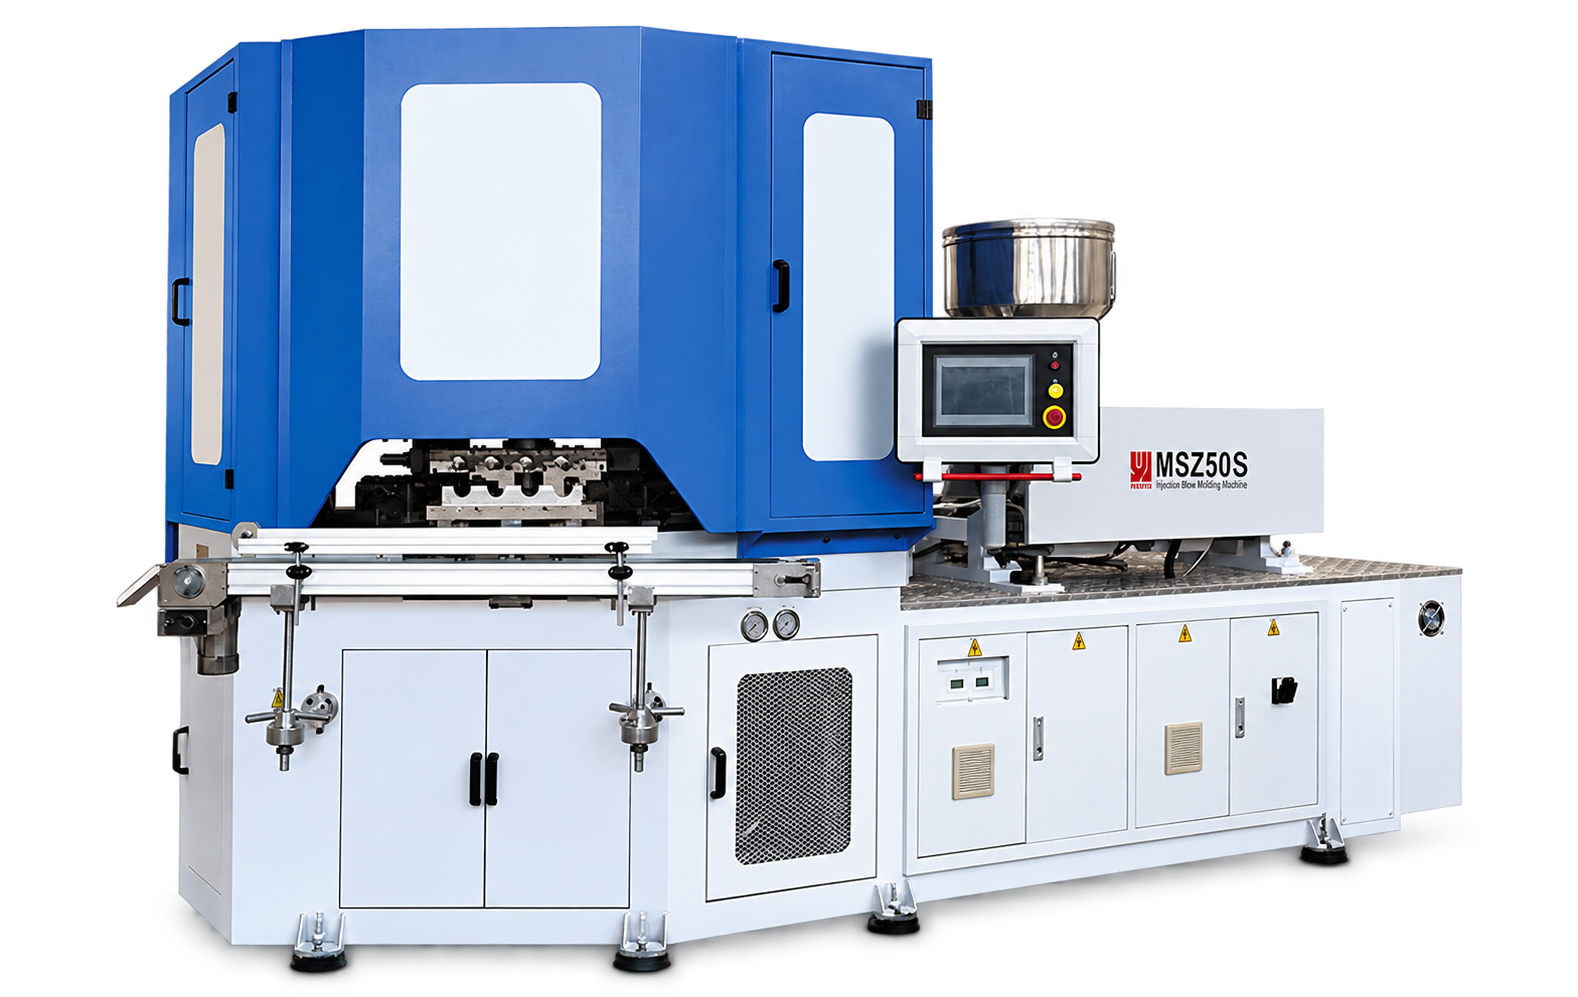
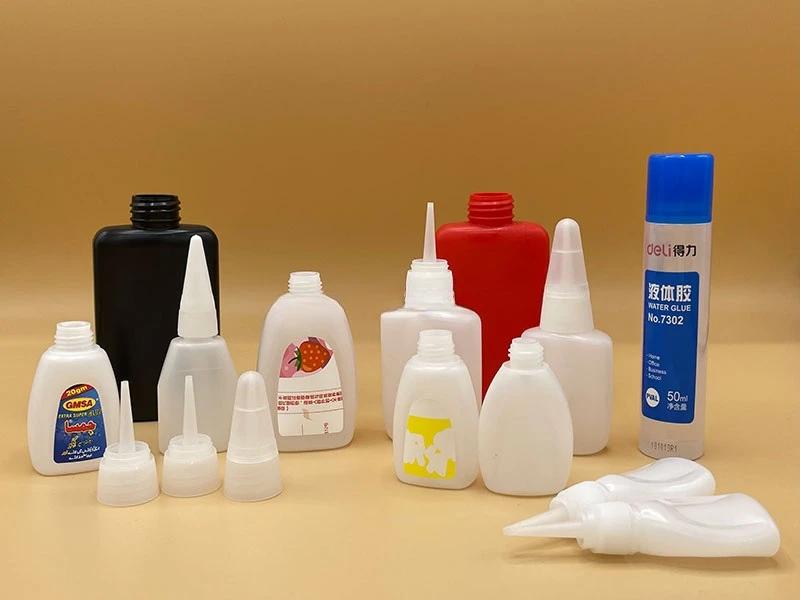
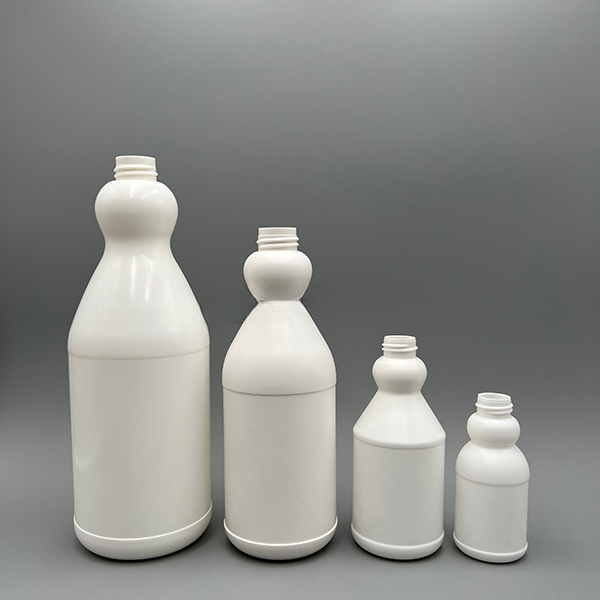
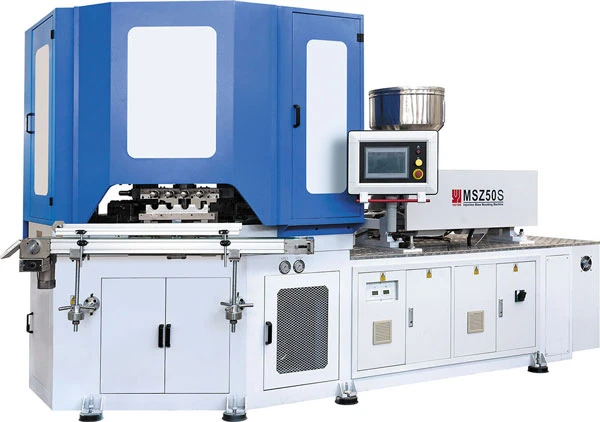
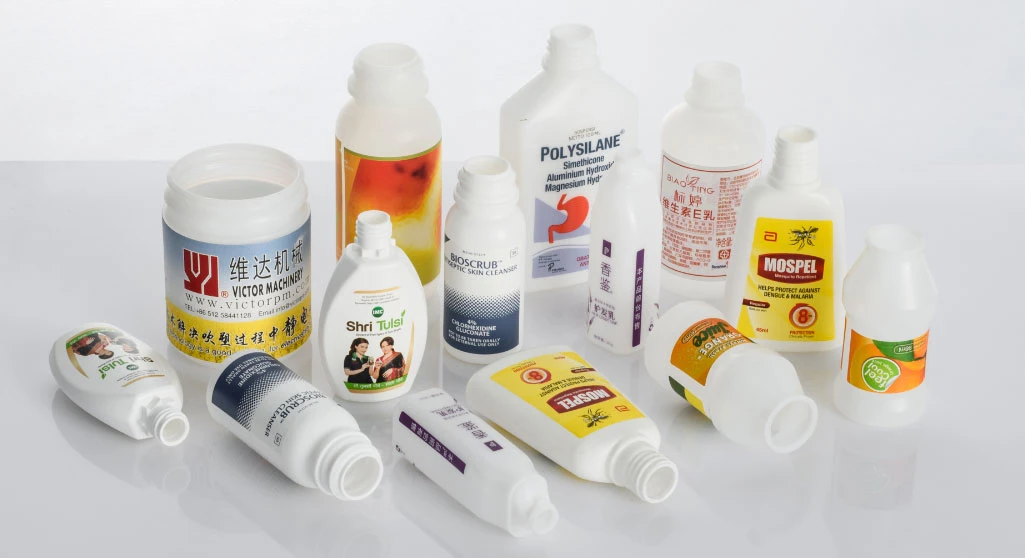
In-mold labeled (IML) bottles on the MSZ50S, the first Victor machine designed for IML, with mold opening, closing and rotation adapted for labeling.
Made on
Production know-how
In-mold labeled (IML) bottles: how we make them
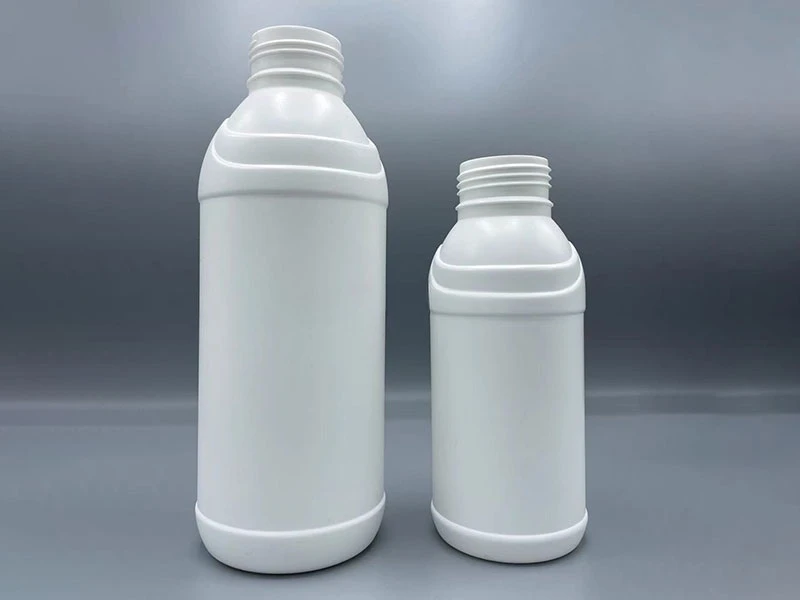
- Without a label the shoulder area was thick and cooled poorly, leaving a white area; increasing shoulder thickness and barrel temperature solved it.
- The label area was very small and hard to position, so the label size was increased to cover the full area – small labels are also difficult for the robot vacuum system.
- IML removes manual labeling of small bottles and increased the customer’s working efficiency by at least 60%.
What to send us
- Bottle drawing, sample or photo
- Volume and material
- Neck finish and closure
- Target output per hour
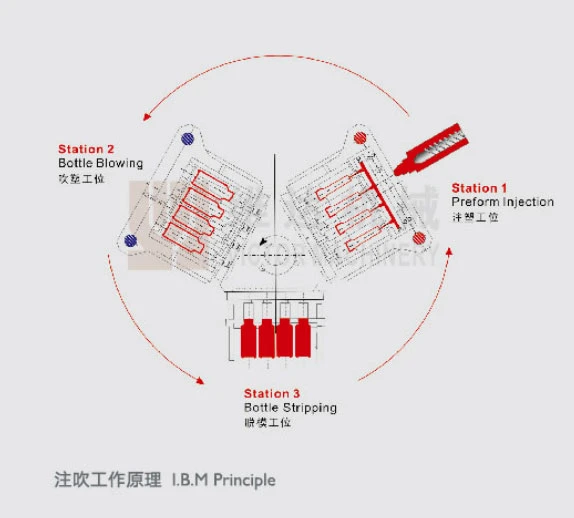
Three-station injection blow molding
One machine, three stations, a finished bottle
- Station 1 · 0°
Injection
The preform is injection molded on a core rod – the neck and thread of the in-mold labeled (iml) bottles are finished here and never change again.
- Station 2 · 120°
Blowing
The table turns 120° and air through the core rod blows the warm preform into the bottle mold. No parison, no pinch-off, no flash.
- Station 3 · 240°
Stripping
Another 120° and the finished bottle is stripped off the rod, ready to pack – no trimming and no scrap, with all three stations working at once.
Machines used